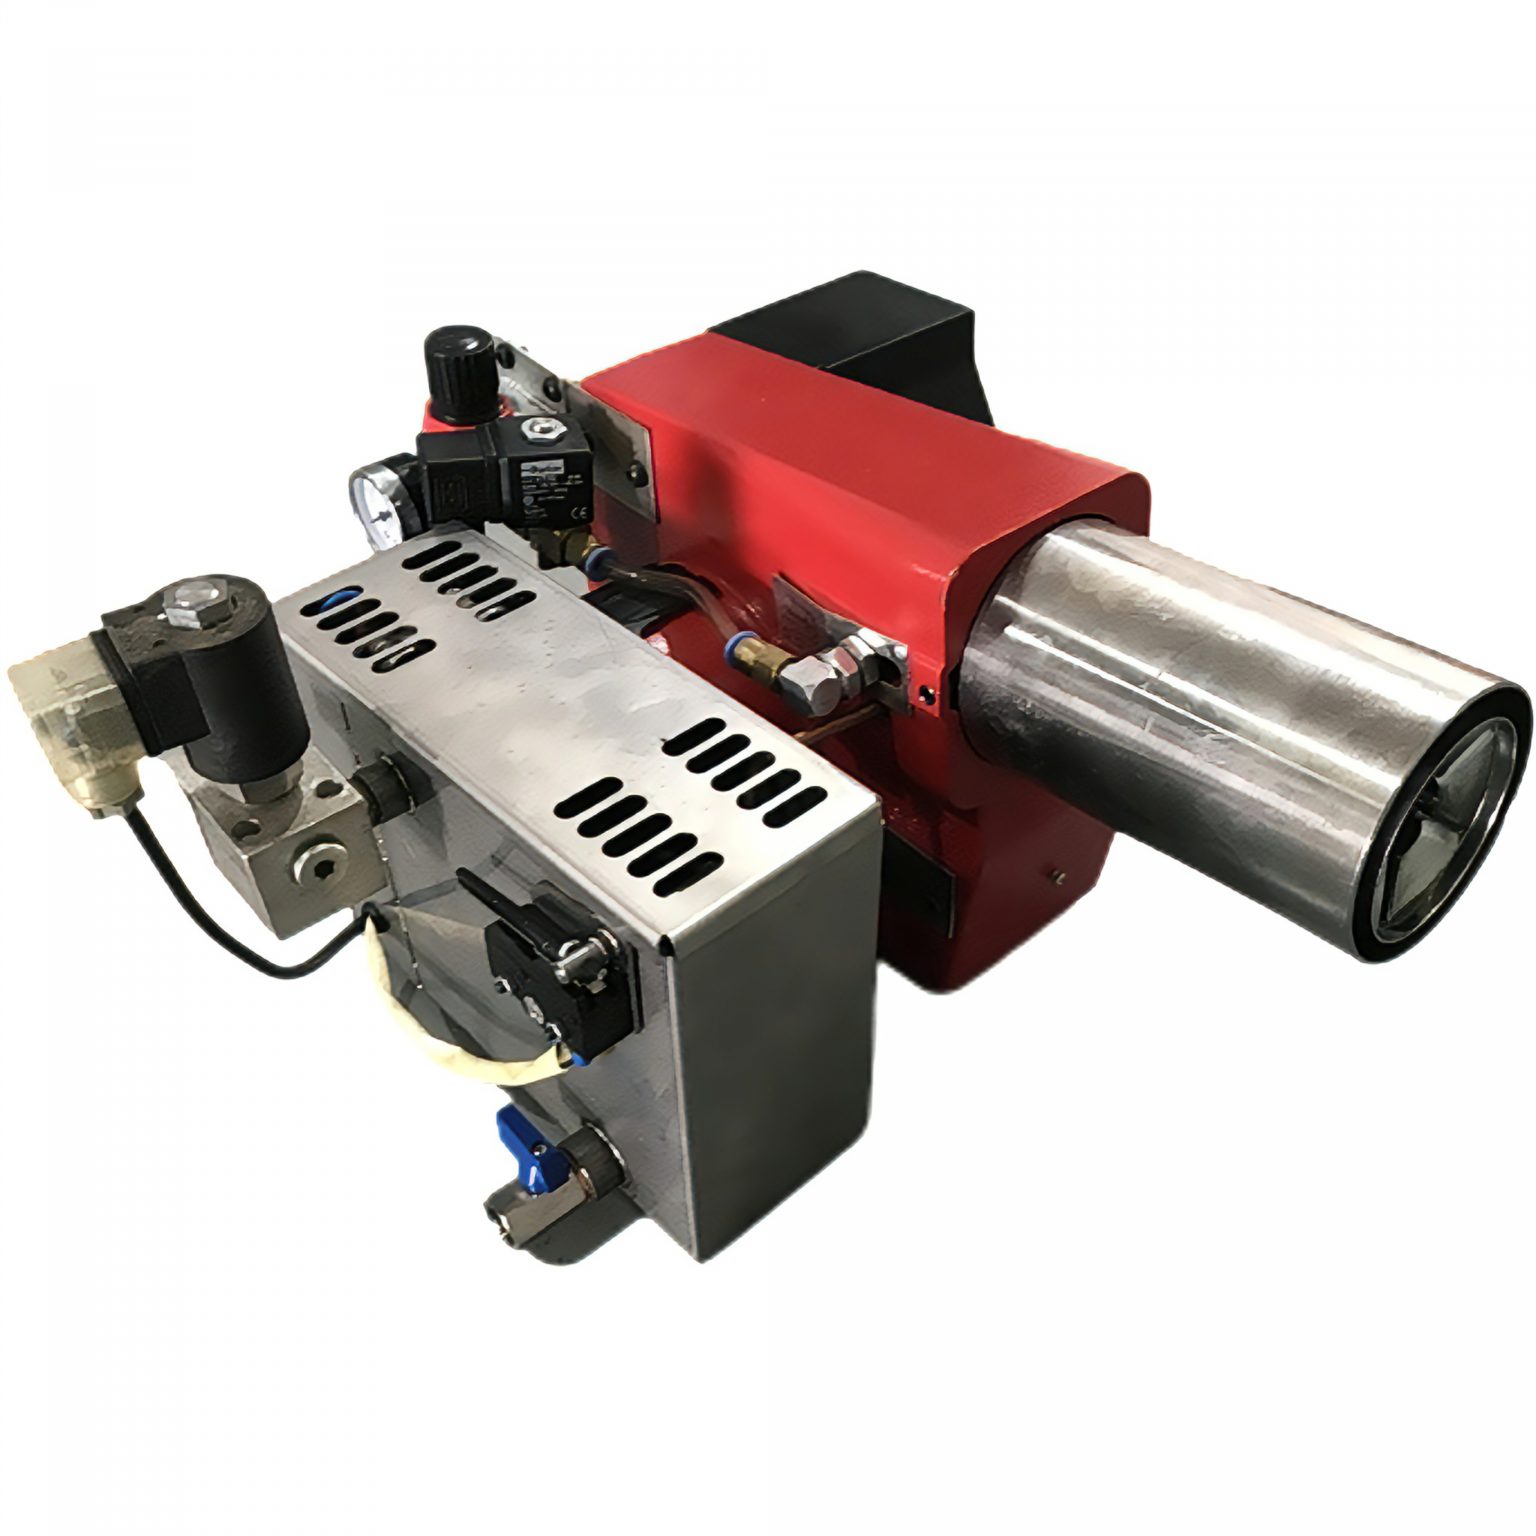
Problem: Systems strain when burners nah fit di work
When yuh run a regional thermal processing plant, di burner mek or break di whole setup. Operators weh try use mismatched burners see fouled heat exchangers, uneven combustion, an’ unplanned shutdowns. Install di right industrial waste oil burner an’ yuh reduce those headaches quick — but pick wrong an’ yuh pay fuel, downtime, an’ regulatory fines.
What really gwan inside di plant
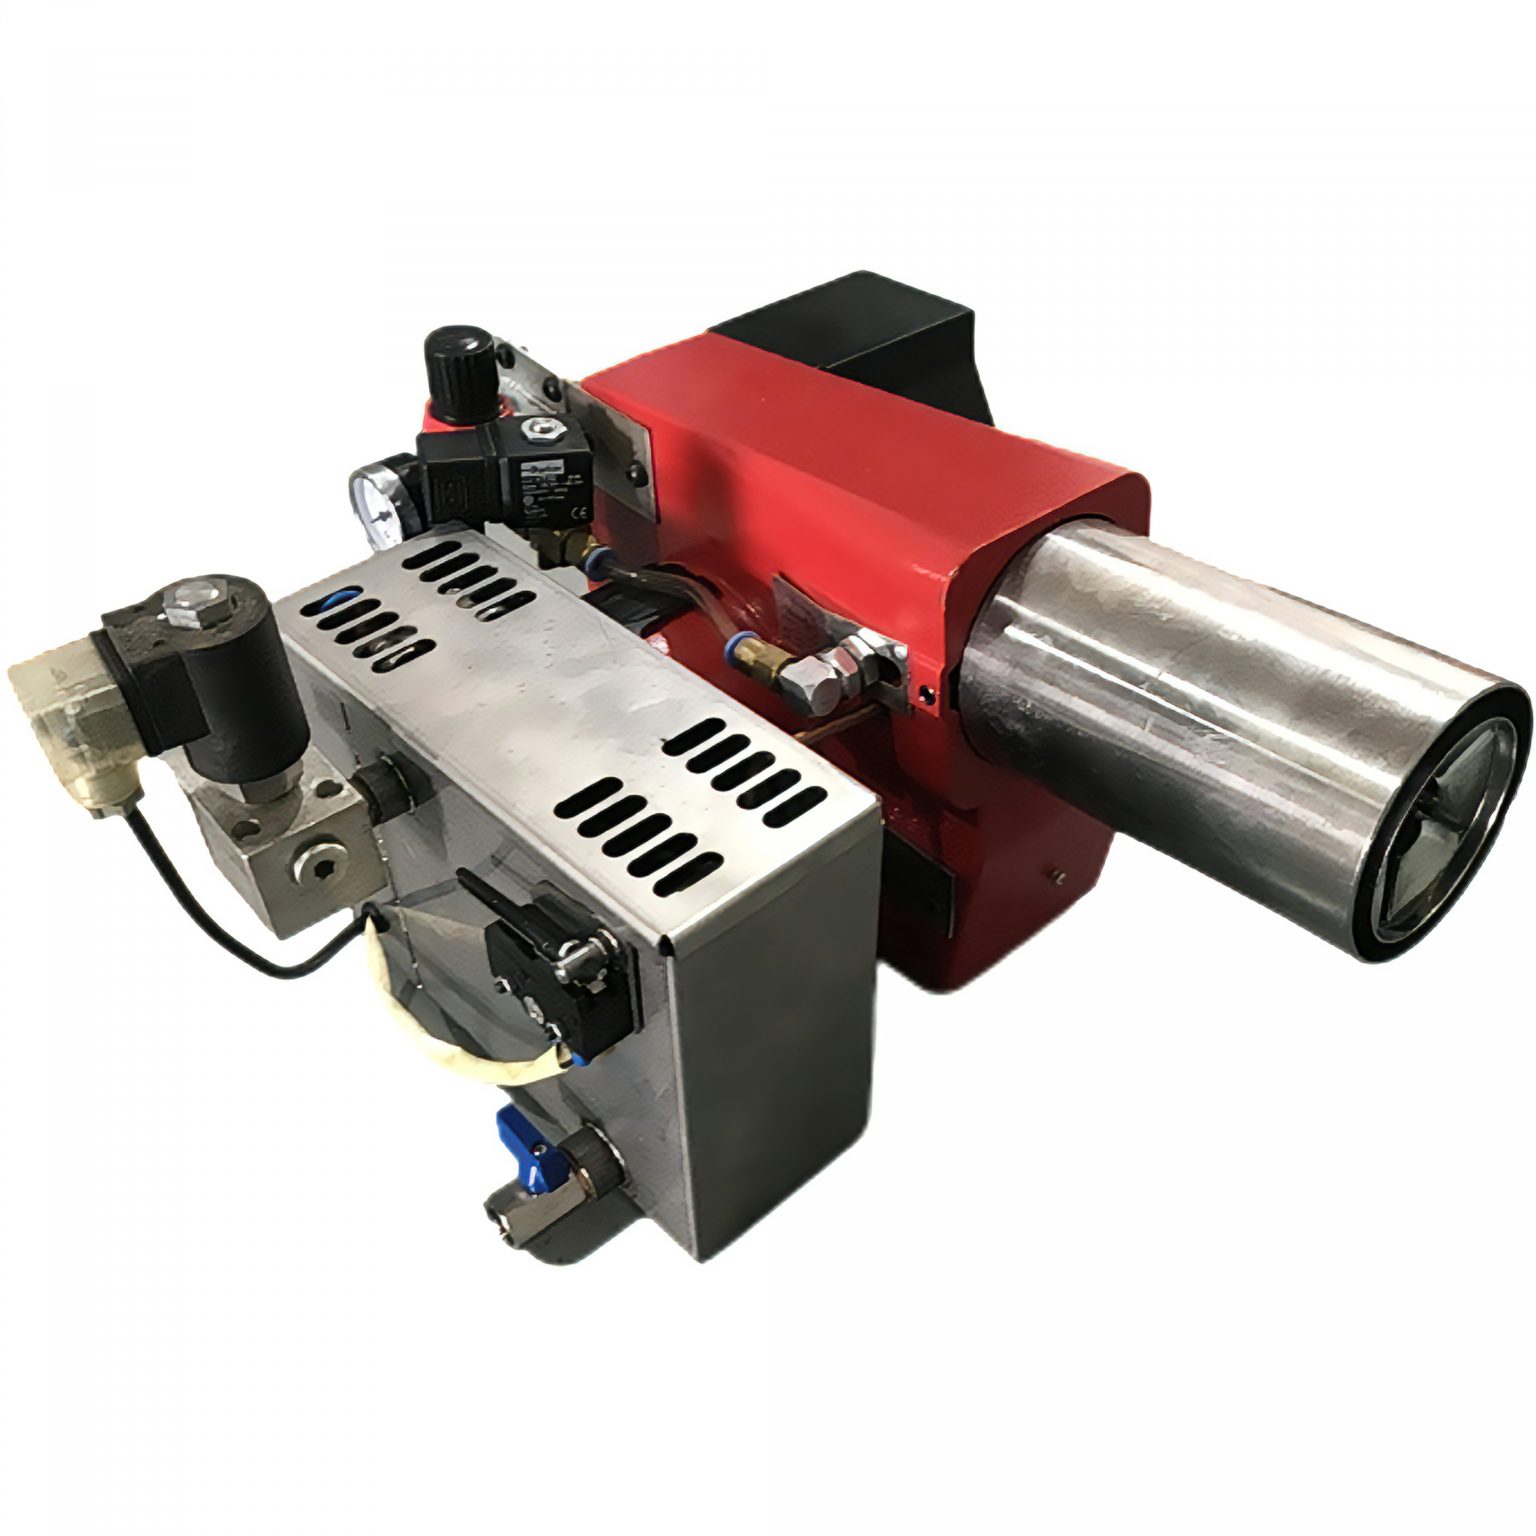
Combustion na simple flame — it’s pressure, atomisation, control logic, and airflow all workin’ together. If injector pattern wrong, heat localize, metal fatigue increase. If control loop lag, temperature swing an’ incomplete burn cause soot and higher CO emissions. Small mismatch in burner turndown or fuel flexibility turn into big maintenance bills.
Where expertise counts: burner capability, not hype
Good burner design give proper atomisation for heavy waste oils, stable flame across load range, and reliable ignition even if oil quality vary. Prioritise measured turndown ratio, nozzle maintenance access, and combustion control with oxygen trim. Ask for field performance data, not just specs handed on paper.
Real-world anchor that show di stakes
Major ports and industrial hubs like the Port of Rotterdam report operational needs for robust thermal units when they process ship-generated residues or industrial slops; operators there prefer systems that can handle variable feedstock without constant supervision. Practical deployments at those hubs illustrate why a dedicated waste oil incinerator design and correct burner pairing cut risk and keep compliance steady.
Alternatives: what folks try and why some fail
Some switch to natural gas or diesel burners to avoid oil variability — that help with emissions control but raises operating cost if gas supply unstable. Others retrofit existing boilers with cheap atomisers; that save upfront cash but cause recurrent plugging and flame instability. The better route balances fuel availability, capital outlay, and long-term serviceability.
Common mistakes operators mek
1) Undersizing: think small burner will do — it cyaah hold load. 2) Skipping pre-treatment: failing to settle water and large particulates clogs nozzles. 3) Ignoring control integration: burner without proper feedback loop produce cycling and soot. 4) Relying on generic spare parts: unique tolerances matter.
Practical checklist before yuh spec or replace
Check fuel variability range and provide sample test results. Confirm turndown ratio matches peak and low loads. Require ease of nozzle change and clear access for inspection. Verify combustion control supports oxygen trim and fault diagnostics. Plan vendor service intervals and spare-part lead times.
Wrap-up: fix di core problem, keep plant steady
When regional thermal systems face variable waste oils, the solution is simple: match a burner engineered for that duty and back it with on-site know-how. That combination reduce soot, downtime, and regulatory exposure, and it’s the practical choice operators look for when they need steady performance — the kind supported by Career Burners in real installations.